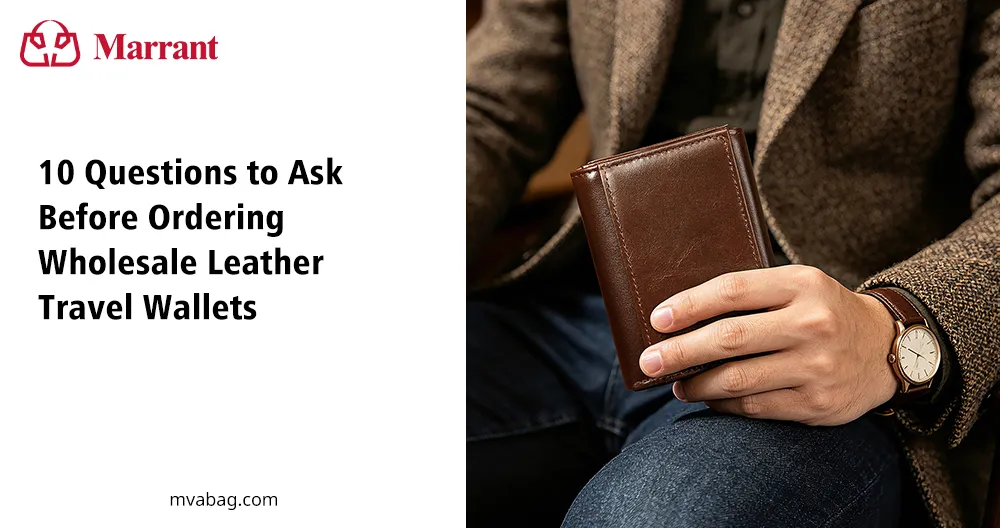
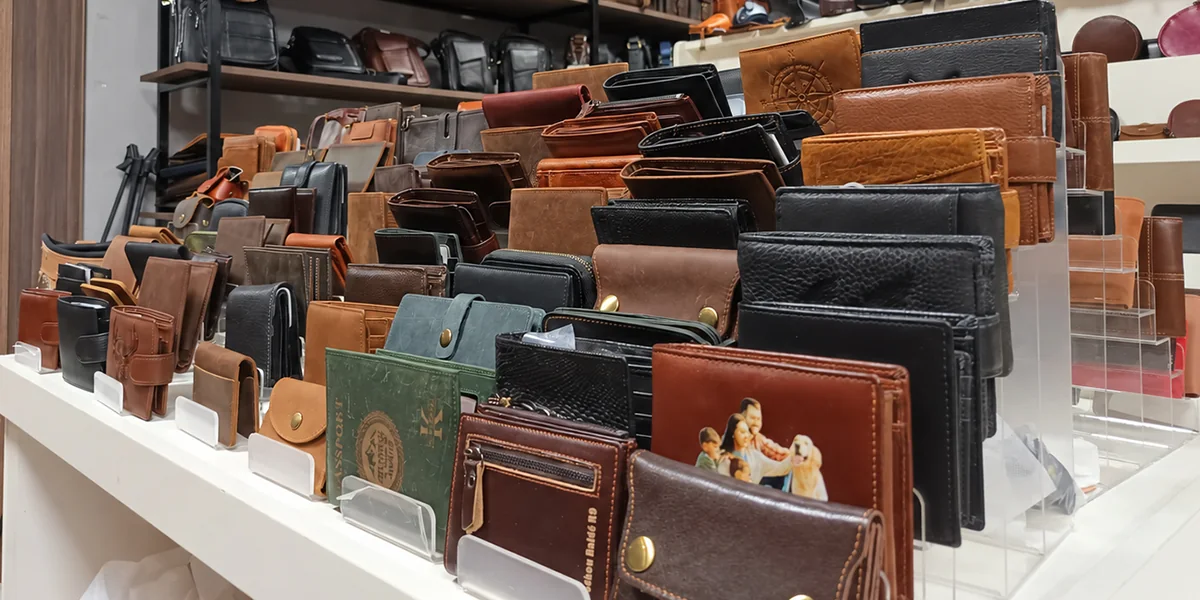
A wallet that looks slim in a supplier’s photo can still feel like a brick in a buyer’s hand. The difference is rarely “full grain vs genuine leather” alone; it is the stack-up math. At Marrant Leather Goods, we treat a bifold like a small engineering problem: panel thickness + card-slot reinforcement + folded gusset + edge paint = final hand feel. Get one layer wrong and the wallet closes like a paperback. Get the compression right and it disappears into a jacket pocket.
What a Custom Leather Wallet Manufacturer Should Specify on Thickness
Buyers often ask for “good leather,” but factories buy by millimeters, temper and yield. For private label leather wallets, the useful conversation starts here:
| Component | Working spec we quote at Marrant | Why it matters | Common failure when ignored |
|---|---|---|---|
| Outer body cowhide | 1.0–1.4 mm, medium temper | Holds shape without cardboard stiffness | Wallet “smiles” open after 3 months |
| Card pockets | 0.55–0.75 mm after skiving at the fold | Lets pockets compress, not bulge | Card slots crack at the mouth |
| Bill divider / gusset | 0.7–0.9 mm where folded twice | Keeps notes from forcing the spine | Center seam splits under load |
| Edge paint zone | Edges reduced to near-even before coating | Prevents a rope-thick rim | Edge paint peels in chips |
| RFID lining | 0.12–0.18 mm shielding fabric, laminated flat | Blocks skimming without adding a foil-board feel | Wallet feels stiff and sweaty |
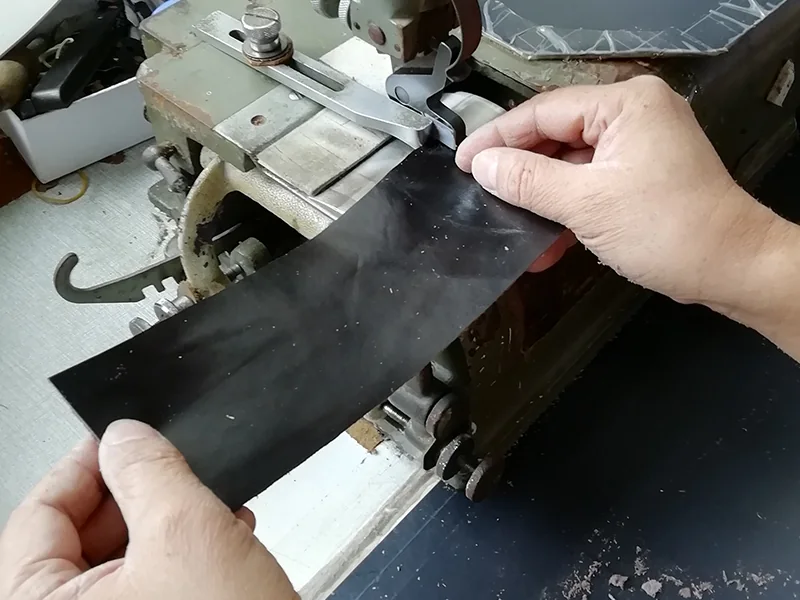
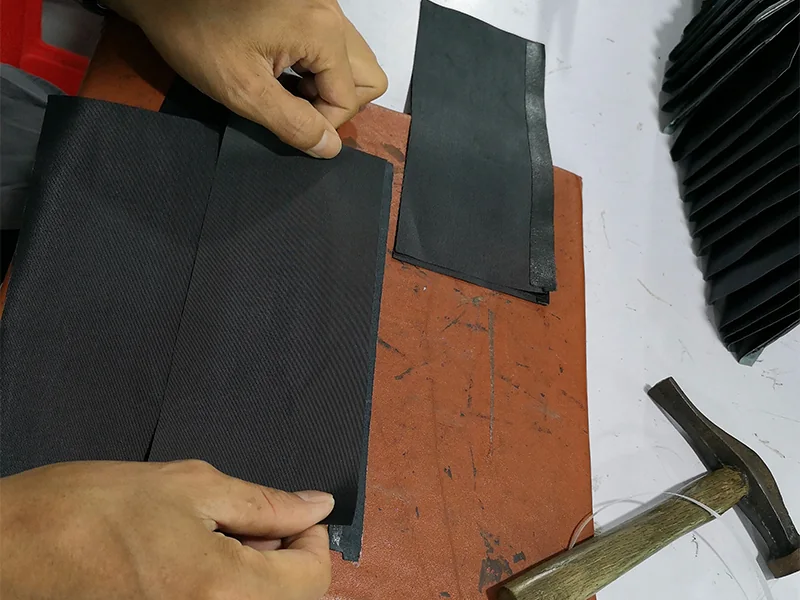
Definition first: skiving means shaving leather thinner at bends and overlaps so stacked layers do not multiply. Turned edge means wrapping an edge instead of leaving a raw cut. Edge paint is flexible coated armor, not a repair for bad trimming.
Our bench target for a standard bifold is 10–13 mm closed thickness with six cards and six notes, measured across the spine rather than the corner. A corner can lie; the spine cannot.
Interior layout: card slots are where margins die
A six-card wallet is not “six rectangles.” Each slot adds a mouth, a reinforcement and a friction point. What the trade floor won’t always say out loud is simple: more slots can mean lower review scores, because cards drag, edges lift and the wallet refuses to lie flat.
Use this layout checklist before you approve a sample from any leather wallet OEM factory:
- Slot pitch: 3.2–3.8 mm between card mouths for smooth draw; under 3 mm feels tight after lining lamination.
- Mouth reinforcement: one thin reinforcement strip only; double strips create a visible speed bump.
- Slot depth: 8–12 mm shallower than card length, with rounded bottom corners to reduce fiber fatigue.
- Bill well: full-width access beats “deep but narrow” for mixed EUR and USD tenders.
- Closed balance: fold the wallet empty; if it springs open, the spine allowance is fighting the pockets.
- One-handed use: the thumb should find the first card in under two seconds. Why design a slot that needs fingernails?
For a custom leather wallet manufacturer, the safest private-label route is to standardize the hidden parts—interlining, slot angles and stitch density—and vary only color, logo and edge paint. That is how a bulk leather wallet supplier protects consistency when the order grows from 300 to 3,000 pieces.
Buyer story: the “slim but strong” trap
A boutique buyer from Hamburg once sent us a photo of a rival wallet: gorgeous Instagram shadow, terrible pocket reality. The sample used 1.6 mm outer leather because “thick equals premium.” We remade the shell at 1.2 mm, skived the fold to 0.65 mm, switched from a shiny hard edge paint to a two-pass flexible coat, and added slim RFID mesh only where cards sit. Closed thickness dropped about 2.1 mm. Return complaints on the next PO fell from the mid-single digits to almost none. Not magic—just refusing to let marketing pick the millimeter.
Logo, packaging and sampling consistency
Logo should follow wear, not fight it. Blind emboss reads rich and ages best on vegetable-tanned panels; hot foil pops for retail but can craze on heavily finished corrected grain; metal plates add weight and can become tiny future loose parts. For wholesale leather wallets, we usually deboss the interior and keep exterior branding quiet.
Packaging is part of QC, not decoration. A recycled kraft box with a fitted insert tells a retailer the wallet will not rub against a zipper in transit. Add a humidity card for sea freight and a batch code inside the flap. Small detail. Extremely useful when a claim lands.
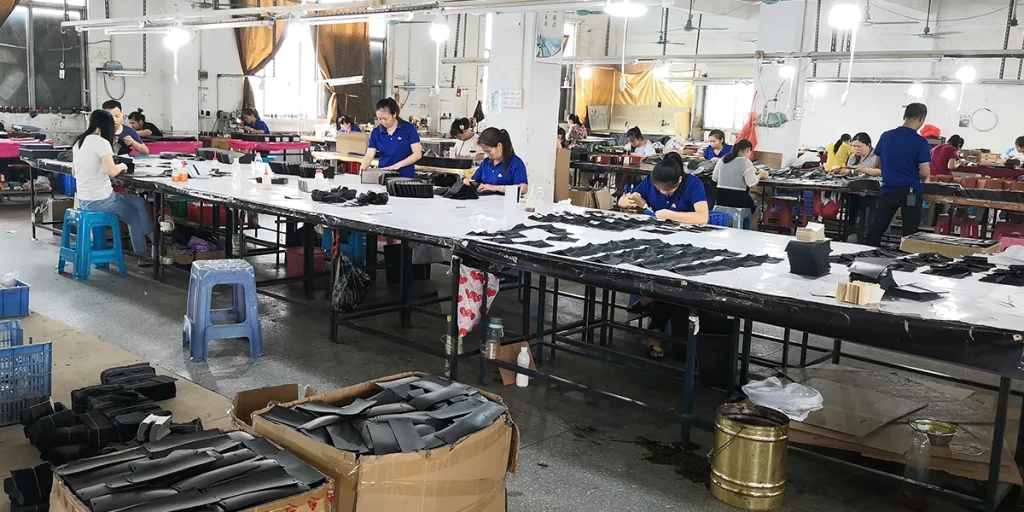
Sampling discipline: approve one golden sample, then measure five checkpoints on every bulk run—closed thickness at the spine, slot-mouth tension, bill-well width, edge-paint adhesion and logo depth. If any one drifts beyond tolerance, stop the line before the cartons multiply.
Approval spec to send any factory: leather temper, outer thickness, skived fold thickness, slot pitch, target closed thickness, edge method, RFID area map, logo process, packaging drop test and AQL for cosmetics.
Browse the build options in our wallet catalog if you want to match a layout to your price band.
Frequently Asked Questions
Q1: What leather thickness should I request for a slim bifold?
Start with 1.0–1.4 mm outer cowhide, then specify skiving to roughly 0.55–0.75 mm at folds and card-slot mouths. “Slim” is controlled at overlaps, not by buying tissue-thin leather.
Q2: Does RFID lining always make wallets bulky?
Only when the shielding layer is laminated like poster board. A targeted mesh, placed only under the card zone, blocks skimming while keeping the bill compartment flexible.
Q3: How do I check bulk consistency before shipment?
Ask for the golden sample plus five measurements per style: closed spine thickness, slot draw force, bill width, edge-paint rub test and logo depth. Consistency is a measured habit, not a promise.
Conclusion
A credible custom leather wallet manufacturer wins or loses in the hidden millimeters: skived folds, disciplined card-slot pitch, closed-spine thickness, flexible edge finishing, selective RFID lining and batch-level measurement. If a factory cannot quote those numbers, the sample may still look beautiful on day one—and complain loudly by month three.